A packaging line can run on time and still create avoidable cost with every shipment. Oversized cartons, unnecessary void fill, inconsistent pack methods, and poorly timed deliveries all create waste that procurement may see as separate line items. This packaging waste reduction case study shows why the best results come from looking at the carton, the production line, the warehouse, and transportation as one operating system.
The scenario below is representative of a product manufacturer shipping high-volume, moderately fragile finished goods to distributors across North America. The numbers are illustrative, but the operating issues are familiar: cartons had been in use for years, damage was within an acceptable range, and purchasing focused primarily on unit price. No one had fully measured the cost of shipping empty space.
Packaging Waste Reduction Case Study: The Starting Point
The manufacturer shipped approximately 220,000 units annually in a standard corrugated carton measuring 24 by 16 by 12 inches. Each product was wrapped in plastic film, centered with loose-fill material, and packed six per carton. The box had been selected when the company carried a wider product assortment. As product dimensions changed, the packaging did not.
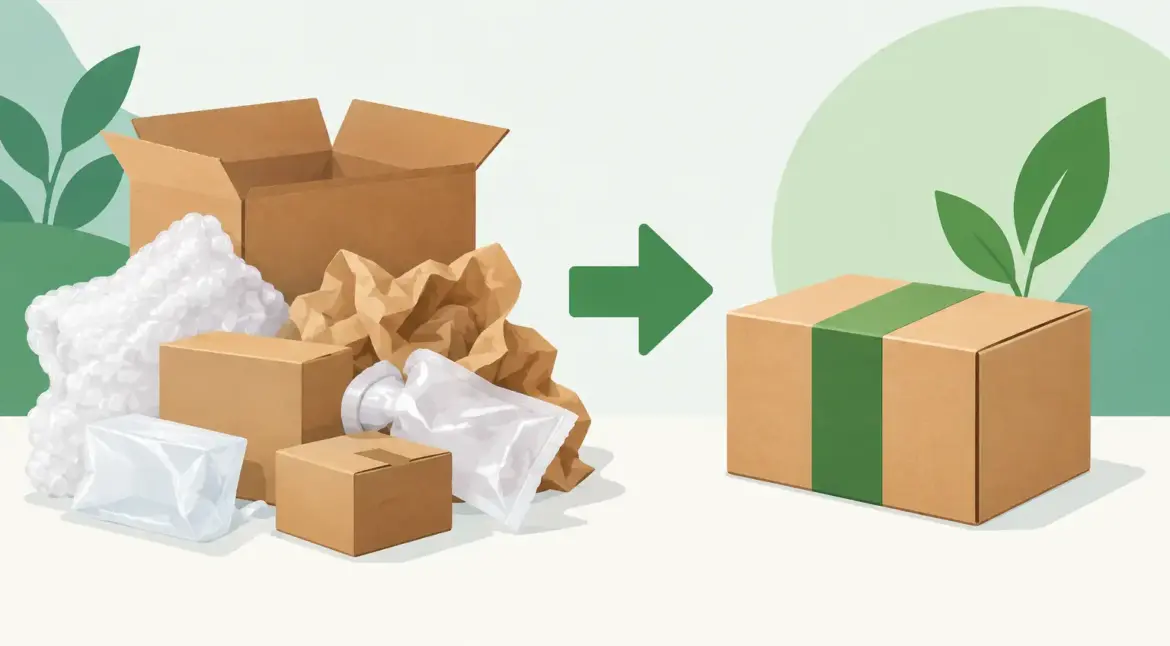
On paper, the arrangement seemed efficient. The carton was readily available, familiar to the packing team, and competitively priced. In practice, it created four operational problems: too much corrugated material per shipment, excessive void fill, inefficient trailer cube, and an inconsistent pack-out process that contributed to occasional damage.
The baseline review did not start with a request to buy a cheaper box. It started at the packing station. The team measured the product, the protective clearance needed around it, the carton dimensions, pallet pattern, warehouse storage footprint, and freight profile. They also reviewed damage reports and watched how operators actually packed the product during a normal production run.
That direct observation mattered. Operators were adding extra loose fill because the product moved inside the carton. Some cartons were taped more heavily than required. Others were underfilled when production ran short of a component. The packaging was not failing because employees were careless. They were compensating for a design that left too much room for variation.
The Baseline Measurements
The review identified an opportunity to reduce carton cube by roughly one-third without changing the number of products per carton. It also showed that the existing board grade was carrying more material than the application required in some directions, while the interior protection was not positioned where the product needed it most.
Before changing anything, the manufacturer established a practical baseline. The goal was not simply to lower pounds of corrugated purchased. The goal was to lower total packaging-related cost while protecting production speed and product quality.
| Measure | Existing Pack-Out | Target for Revised Pack-Out | | — | — | — | | Carton dimensions | 24 x 16 x 12 inches | 22 x 14 x 10 inches | | Carton cube | 4,608 cubic inches | 3,080 cubic inches | | Products per carton | 6 | 6 | | Interior protection | Loose fill | Die-cut corrugated insert | | Pack method | Operator-dependent | Defined work instruction |
The redesigned carton reduced cube by about 33%. That does not mean freight cost automatically fell by 33%. Freight outcomes depend on shipping mode, pallet configuration, lane density, weight, fuel, and how consistently loads are built. But reducing empty space created more options for pallet optimization and trailer utilization.
What Changed in the Packaging Design
The revised solution used a right-sized corrugated carton with a die-cut insert that held each product in a repeatable position. Rather than filling a large open cavity with loose material, the insert provided separation and targeted protection at the points most vulnerable to impact.
This was a material reduction project, but it was not a downgrade. The engineering question was whether the package could use less material while managing the actual distribution hazards the product faced. Carton strength, flute selection, compression performance, stacking conditions, moisture exposure, and handling practices all needed consideration.
For this application, the manufacturer could reduce corrugated usage per shipment because the smaller box had less surface area and the insert eliminated most loose-fill material. The new configuration also improved repeatability. Operators had a defined orientation for each unit, which reduced decision-making at the line and made visual quality checks faster.
A different product might require a different answer. Heavy industrial components may need partitions, pads, or a stronger board combination. Food producers may need packaging that performs in refrigerated or high-moisture conditions. A package that uses less material but raises damage rates is not waste reduction. It simply moves cost from purchasing to customer service, returns, and lost production time.
Packaging Is Only One Part of the Waste Equation
The manufacturer also changed how packaging was supplied to the plant. Instead of carrying a large volume of mixed carton inventory, it shifted to scheduled releases aligned with production demand. This reduced the amount of obsolete packaging on the floor and freed warehouse space previously occupied by slow-moving box inventory.
Just-in-time delivery requires discipline. A plant cannot risk downtime because a supplier misses a delivery window or because demand changes are not communicated quickly. The right partner needs the sourcing capacity, warehouse support, and responsiveness to manage those fluctuations. Time is money, especially when a packaging shortage can stop a production line.
The freight side received the same attention. The smaller carton created a more efficient pallet pattern, and the revised pattern was shared with the warehouse and transportation teams before rollout. That coordination prevented a common mistake: improving the box design while creating an awkward pallet load that hurts handling speed or trailer utilization.
Results That Matter Beyond the Recycling Bin
Using the illustrative annual volume of 220,000 cartons, a reduction of just 0.19 pounds of corrugated per carton would remove approximately 41,800 pounds of corrugated material from the operation each year. Reduced loose fill adds another material saving, but the larger benefit is that the new package controls the product more effectively with fewer separate components.
The improved cube also changes the economics of storage and transportation. Smaller cartons can increase the number of cases stored per pallet location and reduce the number of pallet positions needed for finished goods. For shippers billed on dimensional weight or those frequently cube-constrained in LTL and truckload shipments, that space reduction can have a direct freight impact.
The operational gains are just as valuable. A defined insert and packing instruction can shorten training time, reduce pack-out variation, and make quality problems easier to identify. When packaging is engineered around the actual product and process, the line does less improvising.
The project team tracked performance for several weeks after implementation rather than declaring success on the first shipment. They monitored damage claims, packing time, carton consumption, pallet counts, and feedback from distribution locations. That follow-through is essential because some issues only appear after packages move through multiple handling points or sit in a stacked warehouse environment.
How to Apply This Approach at Your Plant
Start with the packages that move in the highest volume or create the most recurring operational friction. A carton that costs only a few cents more than necessary becomes a meaningful expense when it is used hundreds of thousands of times. A slow-moving specialty box can also deserve attention if it creates storage problems, frequent stockouts, or excess obsolescence.
Measure the product and current pack-out instead of relying on historical specifications. Watch the line, inspect inbound and outbound freight conditions, and ask operators where they add material or spend extra time. Those workarounds often reveal the real packaging problem faster than a spreadsheet.
Then evaluate total cost, not carton price alone. The right comparison includes corrugated usage, inserts or protective materials, labor, line speed, damage exposure, warehouse space, pallet density, and freight. In some cases, a custom die-cut box costs more per unit than a stock carton but lowers total operating cost because it removes labor and reduces damage risk.
Finally, test before full conversion. Run samples through normal production conditions and confirm that the package performs under the stacking, handling, and transportation conditions your product actually faces. A packaging change should earn its place on the line through measurable results.
Waste reduction works best when it is treated as an operating improvement, not a one-time sustainability exercise. The next carton you review may be an opportunity to use less material, move more product, protect it better, and give your team one less reason to fight the packaging at the end of a busy shift.